|
Home » The Finished Part Blog
skip to main |
skip to sidebar
 |
| Stainless Steel Polishing |
Machined stainless steel parts typically have sharp edges, burrs and a matte surface finish. Vibratory tumbling can be used to get a polished finish sometimes even down to just a few Ra surface profile. This is often a multi-step process.
The part on the left is the 'raw' part ready for deburring and polishing. The first step is to deburr and round the edges. This was accomplished using a KM general purpose Ceramic Media. This was a wet process using a solution of Kramco 1010 General Purpose Compound. The result at this point (not pictured) was a matte, tumbled finish with rounded edges.
The second step needed to get the pictured polish (on the right) involved tumbling with a Precision Ceramic Sphere and a solution of Kramco 2020 Burnishing Compound. Generally, a rounder media will produce a smoother finish than an angular media.
This part could be further polished with other tumbling media or hand buffed to a near-mirror finish.
After heat treating and laser cutting stainless steel parts, the edges generally need to be deburred and the surface needs to be cleaned from scale and discoloration prior to polishing. A two-step vibratory tumbling process is normally used to achieve a uniform surface finish.
The part on the far left in the picture shows the burrs and slight discoloration on the edges. The first step was to tumble the parts with a Ceramic Media to get a the uniform, tumbled, matte finish shown on the part in the center of the picture. For this particular part a 2 hour cycle time with a general purpose tumbling compound resulted in the finish seen.
The second step (far right in picture) was also a 2 hour vibratory tumble with a Precision Ceramic polishing (porcelain-type) media and a high lubricity tumbling compound. The surface is improved to a more uniform and brighter finish and the part is ready for a clear coat or further polishing as needed.
 |
| Dirty Cartridge Brass Casings |
In the last post we discussed the differences in performance between vibratory tumbling and barrel tumbling to clean brass cartridge casings. A wet process using a polishing media is a much quicker method to clean brass than dry processes using Walnut Shell Grit or Corn Cob Grit. The test results indicated very similar results in both types of wet tumbling systems.
This post will focus on three different media options for cleaning the dirt and oxidation off the brass. In all three cases, the same solution of Kramco 1030 Mild Acid Cleaner was used and all tests were conducted in a barrel tumbler with a tumble time of 15 minutes.
 |
| Carbon Steel vs Stainless Steel |
The first test compared the differences between Carbon Steel Tumbling Media and Stainless Steel Tumbling Media. It is pretty clear from the picture above that the Stainless Steel was much more effective at cleaning the brass. While this difference would not be expected initially, the reason may have something to do with the characteristic of the Carbon Steel Media to oxidize and possibly the transfer of iron to the brass casings. This reason will be more clear after reviewing the results of the second test.
 |
| Polishing Ceramic vs Stainless Steel |
Once the Stainless Steel Media was declared the winner in the first test, the next step was to compare this heavy, burninshing media with a less dense (and less expensive) media. The above pictures compares the results of a K-Polish Precision Ceramic Media to the same Stainless Steel Media used in the first test. The K-Polish Precision Ceramic Media is a high-alumina, porcelain-type media used commonly in many different tumble polishing applications. Both of these media types are extremely long lasting with the capability for 1,000+ operating hours.
As the results for the Stainless Steel Media and the Precision Ceramic Media are very similar, the decision on which media to use will hinge on the type of equipment being used (many vibratory systems can't handle the weight of steel media), the available budget and the overall desired process.
In conclusion, these tests would seem to indicate that excellent results can be obtained in very short cycle times using either a Stainless Steel Tumbling Media or a K-Polish Precision Ceramic Tumbling Media in either a barrel tumbler or vibratory tumbler.
The far left in the picture shows a laser-cut, stainless steel part with sharp edges and heavy burrs. The goal is to clean up the edges and leave a smooth, polished surface finish. The part will need to be deburred and then polished. This will be a two-step process as an abrasive process like deburring will typically leave a smooth but matte surface finish.
In this situation, the part was first vibratory tumbled with a moderately aggressive Ceramic Media to remove the burrs and discoloration. This process took a couple of hours to result in the smooth, rounded edges and tumbled, matte surface finish shown in the middle part.
The second step used a polishing Precision Ceramic Media to improve the surface finish and brighten the part. The part on the far right have a smooth, polished look after about 2 hours in the tumbler with the polishing media. Overall, a good result without any hand deburring and polishing or manual labor.
Taking machined aluminum parts and polishing to a smooth, uniform surface finish is often a multi-step process. Each step is designed to accomplish a different task. The part above has burrs, sharp edges and clear machine marks. Vibratory tumbling is the preferred process.
Step 1 - The edges are softened and the machine marks are removed using a Plastic Cone tumbling media. This media is selected due to it's lower density (vs. Ceramic Media) and lesser aggressiveness. The resulting surface finish is smooth and uniform. This part could be anodized to a matte finish, powder coated or painted with excellent results.
Step 2 - In order to brighten the part and prepare for anodizing to a higher luster, the part was tumbled with Polishing Precision Cearmic Spheres. While the finish is bright and smooth, the proper shape must be chosen to ensure that a uniform surface finish is achieved based on the geometry of the part.
Question: I am interested in starting a metal polishing
business mainly for car parts. I am wondering if your wet tumblers would be
best and what type of media would be best for polishing aluminium, rough cast intake manifolds? I have polished some by hand using sand papers, air grinders with various deburring bits and abrasive wheels, polishing wheels and compounds. This is very time consuming, dirty and tiring work. I am looking at an easier way! I am also interested in smoothing and peening other cast or forged metal parts for increased strength and durability!
Response: There are a number of different ways to clean and polish auto
parts. Depending on the final finish required and the size, shape and geometry
of the part, the final surface finish can range from a smooth, bright finish
all the way to a near mirror finish.
If parts simply need to be cleaned prior to painting or coating,
blasting with Glass Bead will result in a smooth, satin-like or matte surface finish. If additional polishing is needed, vibratory (or barrel) tumbling with
a Polishing Precision Ceramic or
Stainless Steel Media can produce much smoother, brighter finishes. The key with both processes is to select the proper media shape and size based on the part
and areas of the part that need to be finished. The size of tumbling equipment is based on the size and quantity of parts that need to be finished.
The two pictures below show both the handle area and the blade point on a steel part that has been prepared for cleaning and polishing. The before (left) shows the grinding marks as well as some oxidation (rust) on the surface.

Steel Blade Point

Steel Handle
In order to prepare the steel part for polishing to a mirror finish, a two-step vibratory tumbling process was used. The first step used a fast cutting (KSF Bond) Ceramic Media with a neutral pH compound to remove the machining and grinding marks, clean the surface and create a smooth, matte finish. The second step to achieve the finish on the right was achieved with a polishing (K-Polish Bond) Precision Ceramic Media to smooth out the matte finish and prepare the part for polishing.
Additional vibratory tumbling steps using a harder and heavier media such as Stainless Steel or hand polishing with a buffing wheel will result in a mirror finish.
Many small-run, decorative pewter manufacturers either hand polish or have smaller equipment for polishing cast pewter parts. While we have detailed pewter polishing in a previous post using steel tumbling media, small vibe tumblers generally are not able to handle the weight of steel media.       Before (first) - Polished (second)
These lead-free pewter parts showed rough and dull surface finishes. While the objective was not to completely remove the flashing and produce a mirror-like surface finish, these parts did need to be cleaned and polished. A two step process was used in a small (4 gallon capacity) vibratory bowl. The first step used a general purpose Ceramic Media and a mild acid compound to remove oxidation on the surface and soften/remove the flashing. This resulted in a smooth, matte finish. Instead of using steel tumbling media in the second, polishing step, a Precision Ceramic polishing media was able to bring up a nice shine on the parts in a relatively short cycle time of 2 hours. A neutral pH compound was used to keep the parts clean and bright.
 Removing heavy rust (picture above) off steel can be accomplished successfully using an abrasive blasting process. While effective, the etched finish can be a challenge to polish. A vibratory tumbling process will remove the oxidation and leave a matte surface finish which can be subsequently polished. These steel tubular parts were cleaned and polished in a 2-step vibratory tumbling process first using a general purpose Ceramic Media to remove the oxidation and any pitting caused by the rust (picture below left). The second step involved a Precision Ceramic Sphere to smooth out the surface finish and produce a polished surface finish (picture below right). 
The process of hardening steel using heat treatments, annealing and quenching can produce scale and blackening on the surface. In addition to cleaning and polishing the surface, steel parts often also need to be deburred.  The picture above shows a two step process to clean and deburr the part followed by a polishing step to smooth-out the surface and produce a pleasing surface finish. The part on the left is the unfinished, hardened stainless steel part. Step 1 (middle part) required a vibratory tumbling with a general purpose Ceramic Angle Cut Cylinder to remove the 'burn' marks on the surface and to deburr and round the edges. The result was a matte, tumbled surface finish. The second step (far right) was designed to further clean the surface and result in a smoother part. A polishing Precision Ceramic Sphere was perfect for this part since all the features of the part (i.e., no inside corners) were conducive to a round media.
Cutting steel tubing can produce heavy burrs on the edges and if done wet can lead to rusting on the surface of the parts (picture below).  Rusted Steel Tube Prior to polishing the steel, the part must be deburred and cleaned. The oxidation (rust) will lead to pitting on the surface so an appropriate abrasive media must be used to create a smooth surface finish. Vibratory tumbling the parts with a general purpose Ceramic Media is typically aggressive enough to deburr the edges and remove any pitting from the rust (see left on picture below).  Clean (L) and Polish (R) After the tube was tumbled with a Ceramic Cylindrical Wedge (a good shape for round tube parts), the steel tube was polished with a polishing Precision Ceramic Sphere. This porcelain-type round ball will significantly improve the surface finish and produce a bright polish on the part (see right on picture above). This part is now ready for producing an even higher, mirror-like finish using further mass finishing steps or hand buffing.
Pewter is a soft, malleable metal consisting primarily of tin. Decorative plates, jewelry, figurines and even keys (see picture below) can be made with pewter. Since pewter is so soft, it is difficult to maintain a polished finish on the surface. It is common to treat the pewter design with a black coating that is then polished away from the high spots to produce an exaggerated 3-dimensional effect.  Key Art Co. The black oxide coated parts are vibratory tumbled with Precision Ceramic Spheres and a mild acid cleaner such as Kramco 1030 to 'clean' the high spots. The spheres provide an excellent bright and clean finish without removing the oxide from the interior relief areas of the part. Cycle times can be as short as 10-15 minutes depending on the desired results. If a matte finish is more desirable, a cutting/abrasive version of the Precision Ceramic Spheres can be used. To remove more of the oxide, a triangle media is ideal.
 Before This small polyamide, thermoplastic resin, hardened part had a rough surface finish as well as flashing that needed to be removed. The challenge in deflashing and polishing plastic parts is to choose a media that will be aggressive enough to remove enough material to create a smooth finish without scratching or etching the surface too much so that the part can be polished successfully.  After A two-step process was used to first de-flash the part and then polish the surface. The first step involved vibratory tumbling with a Precision Ceramic Fast Cutting Sphere to remove the flash and smooth the surface. This shape and bond (formulation) of media provided good cutting action (deflashing and edge rounding) but not the rough, 'tumbled' finish normally associated with angular shaped media. The part was then polished with a Precision Ceramic Polishing Sphere. Again, this shape provided the best polishing action and left the part with a near-mirror surface.
 Deburred Deburring and polishing aluminum is almost always a multi-step process. The aluminum part pictured above was deburred using an aggressive Ceramic Media in order to achieve a heavily rounded edge. Using an aggressive media, of course, makes the polishing process much more difficult since the surface finish after deburring will be a rough, matte finish.  Polished After tumbling with a Precision Ceramic Media (2nd picture above), the surface finish is much smoother and brighter. While this would certainly not be considered a mirror finish - which is extremely difficult to achieve on aluminum with a tumbling process alone - the part is ready to be painted or anodized to produce a beautiful result. In addition, the part can be further burnished using a dry tumbling process with a media such as Walnut Shell Grit, Corn Cob Grit or even a Hardwood Media and a polishing cream.
Manufacturers of ammunition have been working overtime to try to meet the recent surge in demand. Due to lack of supply, many shooters have been doing more and more re-loading. The traditional process of dry vibratory tumbling with Walnut Shell Grit or Corn Cob Grit continues to be the primary method for cleaning the cartridge brass. While this process works well for newer brass, heavily oxidized brass can be more 'stubborn' using this process. Using the same dry vibratory tumbler (assuming it is water-tight) with a Precision Ceramic Media can clean even severely oxidized and soiled brass. In addition, the cycle time can be as little as 15 minutes versus the 12-24 hours for dry tumbling. The key is to use the proper shape and size media for the brass you need to tumble in combination with a cleaning compound such as Kramco 1030. To see a great before and after example, click to this Finished Part post.
Plating involves the deposition of thin films of metal onto other surfaces. Tumbling plated products can be a challenge to achieve the desired results without removing the thin metal film.   The picture on left shows a silver plated part with a dull surface finish. The desired shiny, polished finish on the right was accomplished with a vibratory tumbler. A precision ceramic polishing media was used since this media has no abrasive and is high density allowing for a short cycle time (1 hour). In addition, a high lubricity, pH balanced burnishing compound was used to produce a high shine. This process produced a customer-approved surface finish and did not remove the plating - even on the edges and corners.
After molding these decorative aluminum plates are treated with a black carbon/oxide that then needs to be removed to create a striking, shadow effect. 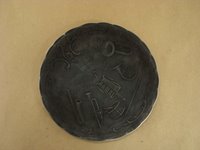 Before tumbling  After tumbling While it might seem that an abrasive media with lots of corners (like a triangle or angle cut cylinder) would be best to remove the carbon, this part was vibratory tumbled with Precision Ceramic Spheres and Kramco 1030 to remove the black coating from the high spots. This combination of round media and mild acid cleaner significantly enhanced the 3-dimensional effect desired by the customer.
We received a post a couple of years ago about polishing body jewelry in a vibratory tumbler. While very similar to other jewelry there was a concern about the size of the parts and the threads at the ends. The recommendation was to polish the parts using a Precision Ceramic media to be able to get into the finer areas of the part without damaging the threads. Steel tumbling (while also effective) might roll the thread edges. A simple but effective result.
Bringing machined aluminum into a highly polished finish is a multi-step and sometimes challenging process. The first step is to tumble (vibratory usually works best) the parts in an abrasive media such as a Plastic or Synthetic Media. Using as round a media shape as possible - cones vs triangles - will result in a smoother finish producing a better end result. The second step is a polishing step using a Ceramic Media. Either an Angle Cut Cylinder or a Precision Ceramic Sphere will produce a smooth surface finish - again rounder is better. In order to burnish the surface (if necessary), a third step can be to dry tumble the parts with a Walnut Shell Grit possibly treated with a fine abrasive such as jeweler's rouge. It is important to make sure that the chemical compounds you use will not attack the aluminum. Depending on the final finish required, a small amount of hand polishing may be needed.
The art of mass finishing really shows itself when trying to select a tumbling media. Media is the material ('stones') that parts are tumbled with in either a vibe or barrel tumbler. The types of media available are as varied as the parts that can be tumbled in a mass finishing process. Ceramic Media is available in bonds or formulations that range from super aggressive, cutting to non-abrasive polishing. The most popular preformed shapes are triangles, cylinders and variations of these shapes. Ceramic media is typically used with hard metals such as steel. Softer metals such as aluminum can be tumbled with ceramic media but care should be taken so the process is not too aggressive. Precision Media is a high density version for specialty applications. Plastic Media and Synthetic Media have a lower density and are thus less aggressive than ceramic media. These media are typically used with aluminum, copper, brass and other soft metals. Popular preformed shapes include cones, pyramids and wedges. Steel Media is used primarily for polishing and burnishing operations in barrel tumblers. Some vibes can be set-up to handle the weight of the steel media which is 3-5 times as heavy as the other preformed shapes. Other types of tumbling media include Hardwood Media (dry tumbling of wood and some plastic parts), Aluminum Oxide (surface finishing and etching), Walnut Shell (burnishing) and Corn Cob (burnishing) as well as many other specialty media. Choosing the proper type, size, shape and bond is critical to making sure that the required finishing is achieved. Common problems include excessive media wear, poor and/or inconsistent surface finish, too much (or too little) edge rounding and media 'jamming'.
|




 Posts